

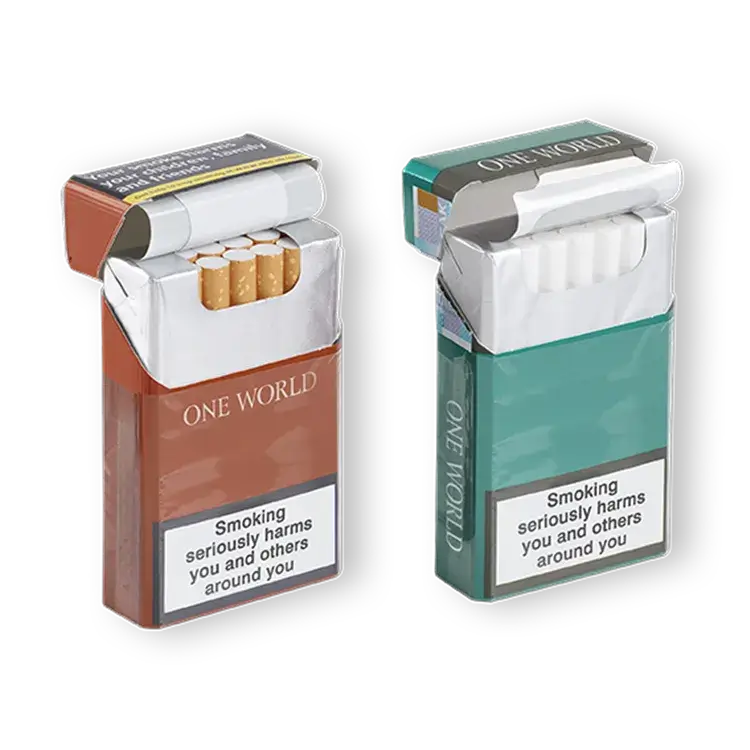
Cigarette Inner Frame & Box Lining Paper
The cigarette inner frame sits inside the pack and does more than it appears to. It keeps the pack rigid through transport and everyday use, and it shields the cigarettes from humidity and compression so the tobacco holds its flavour.
Material
Inner frames are made from sturdy cardboard or specialised paper. White cardboard and aluminised paper are common choices, selected for durability, moisture resistance and cost. Recyclable and biodegradable paper options are used where the market calls for them.
Printing and coding
- QR codes, serial and random numbers, verification codes and barcodes
- TTR, UV or laser numbering
- Sheet or roll supply
Quality and certification
Production is held to ISO 9001, ISO 27001, RoHS and IHMA requirements. Buyers also refer to this component as cigarette inner paper, liner paper, inner foil, pack interior paper or box lining paper.
Ordering
Send us the pack format, the numbering scheme and the roll or sheet size you need.
Cigarette inner frame board — typical industry reference
The figures below are typical industry reference values for this product category. They are not measured values for your order. The final board grade and the slitting specification are set together with your engineers against your cigarette format and your packing line.
| Base board | White-lined board, full virgin pulp with no recycled fibre; coated front, sized back |
| Board grammage | Commonly 215 / 220 / 225 / 230 / 240 / 250 g/m²; design values for the category sit around 220–260 g/m² |
| Grammage tolerance | Typically within ±3.0% of the design value; most samples within ±3 g/m² |
| Roll width vs cigarette format | 74–77 mm slim · 87–90 mm medium · 94–96 mm regular · 111 mm double-medium |
| Types | Plain white board, printed, registered (print-to-position), transfer-metallized, foil-laminated, vacuum-metallized, embossed |
| Converting route | Gravure or offset printing → foil stamping → creasing (U-crease + dotted line) → die-cutting → slitting / rewinding |
| Supply form | Rolls are the dominant form; sheets are used only for special and odd-shaped packs |
| Warp | Controlled below 5 mm — one of the recognised make-or-break properties on the packing machine |
| Core inner diameter | Tolerance typically ±0.5 mm |
Creasing reference (for 230–250 g/m² board)
- Crease width 1.0–1.2 mm.
- Crease depth 0.16–0.18 mm at the glue flap and 0.14–0.15 mm elsewhere; glue-line depth about half the board thickness.
- Crease stiffness is mostly held at 40–70 g·cm, with the break/turn ratio held at 15–35 g·cm. The stiffness target differs by pack: roughly 50–60 g for slim packs and 60–80 g for a standard hard pack.
- Board moisture: 8–10% before printing, 6–8% in the finished product. Below 6% the board turns brittle and the crease cracks (“bursts”).
What decides whether it runs
- Warp and moisture control — warp and moisture are the two properties that decide how the board feeds and creases; batch-to-batch grammage variation should stay inside about 1%, and two batches running more than 1% apart should not be mixed.
- Creasing and die-cutting — the U-crease and the dotted line have to hold through the fold without cracking the print.
- Print rub resistance — the printed layer must survive handling up to the die-cutter.
- Solvent residue — the reference test method is headspace gas chromatography–mass spectrometry (HS-GC/MS).
Standards and compliance
This product is made to the current category standard together with our internal control standard and the applicable food-contact requirements. Food-contact declarations and a solvent-residue (HS-GC/MS) test report are provided on request.
Request an inner frame quotation
Tell us the cigarette format, the board grade and the slitting you need. Our engineers reply with a specification and a quotation — usually within 24 hours.
Pricing available on inquiry — MOQ varies.